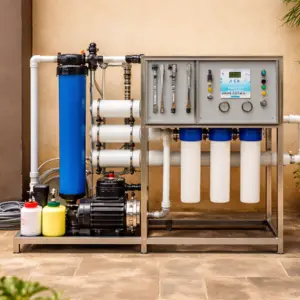
The 500 LPH Industrial Reverse osmosis plant takes out all the contaminants and impurities from water and makes it fit for drinking purposes. When water is passed through a semipermeable membrane then it filters out all kinds of harmful impurities from it. It removes organic and inorganic solvents lead, dirt, bacteria, silt, Insecticides, Chloramine, and Turbidity etc.
It is designed to supply purified drinking water for restaurant, schools, Nursing Homes, Colleges, building, mall, complex etc
Main Feature of 500 LPH RO Plant Product:
- Low maintenance and Easy installation
- Removes non-essential and corrosive salts, salts, minerals and other impurities metals & chemicals
- Easy to operate & cost-efficient
- High production capacity
- More Reliable & Durable
Description
"Greenly: Seamlessly Automated RO Plant Solutions''
Greenly offers the best 500 LPH RO plant. It Provides 500 Liter of water per hour for drinking purposes. With a deep knowledge of various aspects, we are prominent in rendering a quality range of Industrial RO (Reverse osmosis) plants. All products are designed under the supervision of experts. We are using international standard accessories to make quality products. We deliver the good quality products at the good price in Industry. Customer satisfaction is our main motto so we customized plants according to the need or requirements of our clients.
500 LPH-Semi-Automatic RO-TDS upto 1500-Recovery 50 % is part of the Greenly RO water plants range, made by Greenly in Ambattur, Chennai.
Greenly manufactures reverse osmosis plants in Ambattur, Chennai — from 25 LPH home units to multi-stage industrial skids — sized on your water report, not on guesswork.
Need help choosing?
Send us your requirement, site details and quantity. For water treatment products, a recent water report helps us confirm the right model. We reply on working days, 10:00 am – 5:30 pm.


Reviews
There are no reviews yet.