Industrial RO plant purify the raw water and take out all the Contaminants out from impure water like Organic a7 inorganic impurities, harmful chemicals calcium, magnesium, Chlorine, Sand, Insecticides, Viruses, Fungi, Chloramine, Silt etc.
Water which is purified through industrial RO plant used for various kind of application like:
- For Drinking Purpose
- Hotels and Restaurants.
- In Pharmaceutical industries
- In Metal industries
- Colleges/Offices
Description
"Greenly: Seamlessly Automated RO Plant Solutions''
We manufacture both types of reverse osmosis plant semi-automatic or fully automatic according to the need of clients and their requirements. These types of RO plants are acclaimed for their ease of operation, operation fluency, flow per rate capacity and much more.
Work flow of 500 LPH RO plant:
- Generally there are 5 steps of water purification methods which are explained below:
- First, the water is filtered through sand filtration
- After the sand filtration process, the water passed through activated carbon beds, to remove the foul odor, color and carbon from raw water.
- Now Hard water is softened
- When the water is softened add a scale inhibitor in it.
- At the end water is passed through cartridge filters to remove all kinds of leftover particles.
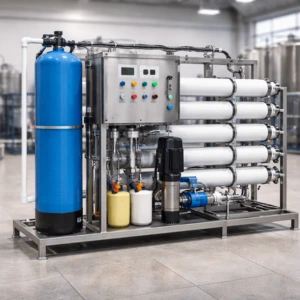
500 LPH-Automatic RO-TDS upto 1500-Recovery 50 % is part of the Greenly RO water plants range, made by Greenly in Ambattur, Chennai.
Greenly manufactures reverse osmosis plants in Ambattur, Chennai — from 25 LPH home units to multi-stage industrial skids — sized on your water report, not on guesswork.
Need help choosing?
Send us your requirement, site details and quantity. For water treatment products, a recent water report helps us confirm the right model. We reply on working days, 10:00 am – 5:30 pm.



Reviews
There are no reviews yet.