As we all know, raw water is not suitable for drinking purposes because it contains harmful bacteria, virus, dissolved impurities and other contaminants. So we need industrial RO plants which purify water and make water fit for drinking purposes.
Benefits of 250 LPH RO Plant:
- It removes toxic salts, metals & chemicals from water
- Making water safe for drinking purpose
- Easy to operate and install and cost-efficient
- Rejects harmful bacteria, proteins & other particles
Features of 250 LPH RO Plant:
- Product is Robust in design
- Highly efficient and environment friendly product
- Long lasting performance
- Less electricity consumption
Description
"Greenly: Seamlessly Automated RO Plant Solutions''
Our main aim is customer satisfaction, that’s why we always deliver high quality products. Which are designed or manufactured under the guidance of experts. Greenly always uses international standard accessories to maintain the quality of product. Our all products are robust in design and durable.
Why Greenly better than others
- Fully efficient product so negligible maintenance required.
- We provide excellent Water Recovery rate of more than 70%,
- Always use International Standard accessories to manufacture products
- Our products have longer durability
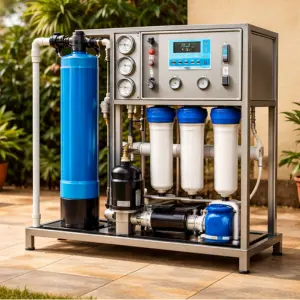
200 LPH-Automatic RO-TDS upto 1500-Recovery 70 % is part of the Greenly RO water plants range, made by Greenly in Ambattur, Chennai.
Greenly manufactures reverse osmosis plants in Ambattur, Chennai — from 25 LPH home units to multi-stage industrial skids — sized on your water report, not on guesswork.
Need help choosing?
Send us your requirement, site details and quantity. For water treatment products, a recent water report helps us confirm the right model. We reply on working days, 10:00 am – 5:30 pm.



Reviews
There are no reviews yet.